Engineering Challenges. Practical Solutions.
Detailed technical summaries of how our engineering team solved severe seal failures, reverse engineered obsolete shafts, and increased rotating equipment MTBF.
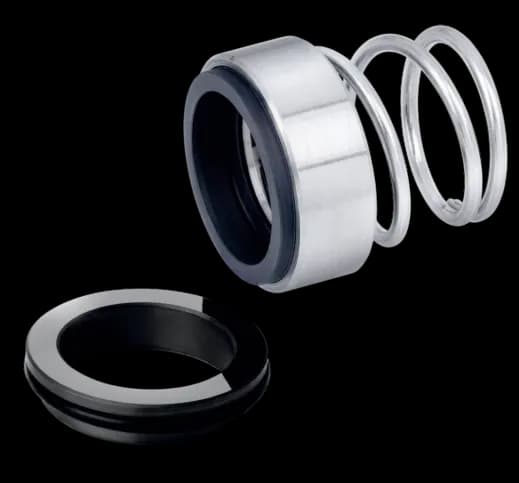
Slurry & Acid Mechanical Seal Retrofit for Chemical Processing Plant
The facility experienced frequent mechanical seal failures on sulfuric acid transfer pumps (failing every 6 to 8 weeks) due to face thermal distortion, crystalline solids buildup, and chemical attack on secondary elastomers.
Eliminated chronic weekly seal leakages and extended the continuous operating life beyond standard turnaround cycles without unpredicted process interruptions.
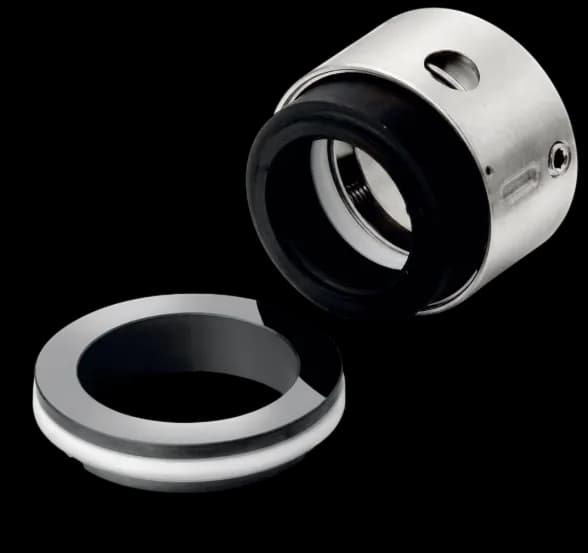
Precision Reverse Engineering of Multi-Stage Boiler Feed Pump Shaft
A utility provider faced a 26-week OEM lead time for an obsolete 7-stage boiler feed pump shaft, risking extended boiler downtime during scheduled peak power generation.
The pump was successfully reassembled and dynamically balanced ahead of schedule, with vibration levels falling well below ISO 10816 Class II limits.
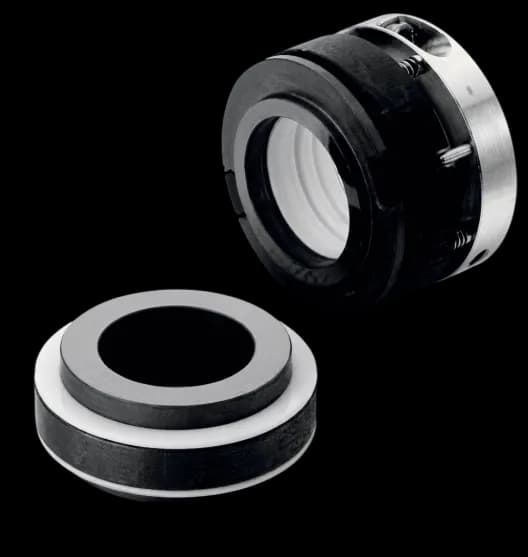
Non-Metallic Anti-Galling Wear Rings for High-Flow Wastewater Pumps
High-volume raw sewage pumps suffered rapid internal clearance expansion due to abrasive grit, leading to severe internal recirculation, drop in flow rate, and excessive energy consumption.
Restored pump hydraulic output to design head-flow curves and reduced kilowatt-hour power consumption per megaliter pumped.
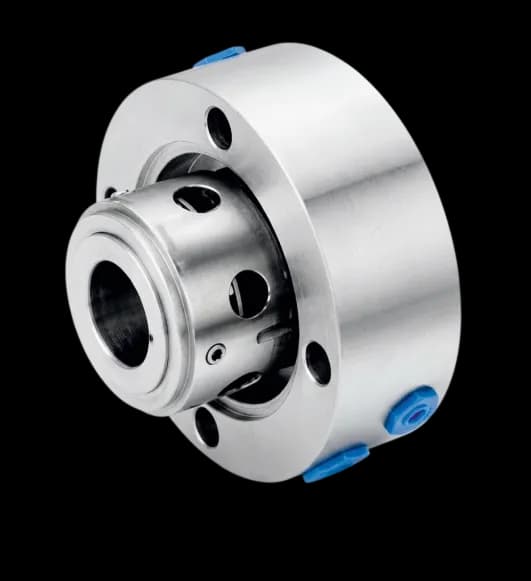
28% High-Chrome Impeller & Casing Upgrade for Mineral Tailings Pumping
Severe particulate erosion on mineral slurry pumps resulted in impeller vane perforation every 45 days, causing severe gland seal dilution and frequent unscheduled outages.
Wear life increased significantly between inspection intervals, streamlining scheduled plant maintenance shutdowns.
Facing a Similar Rotating Equipment Challenge?
Our engineering team can evaluate your pump operating conditions and recommend tailored component upgrades.